

How is PP air filter material tested?
PP (polypropylene) air filter media, with its advantages of acid and alkali resistance, low resistance, and ease of processing, is widely used in fresh air systems, automotive air conditioning, industrial dust removal, and other fields. Its filtration effectiveness and operational reliability require validation through scientific testing. This article outlines key testing items, methods, and criteria—from fundamental metrics to specialized scenarios—centered on the core performance of PP air filter media, providing reference for enterprise selection and quality control.
Appearance Quality Inspection
Primarily inspects the color uniformity, mesh structure integrity, and surface defects of the filter material:
- Color must meet design requirements with no noticeable color variation within the same batch;
- Mesh should be uniform, free of burrs, breaks, wire overlaps, or severe flattening;
- Edge trimming must be neat, with flash at the mesh frame junction ≤2mm (≤1.5mm for high-density mesh), and no delamination or brittle fractures.
Structural Dimension Inspection
For different types of PP filter materials, inspect weave density, mesh wire diameter, and dimensional tolerances:
- Weave Density: Flat injection-molded: 32 threads/inch warp, 34 threads/inch weft; Pleated injection-molded: 39 threads/inch warp, 33 threads/inch weft; High-density: 48 threads/inch warp, 37 threads/inch weft, etc. Tolerance: ±2–3 microns;
- Mesh wire diameter: Standard mesh: 0.20 ± 0.02 mm; High-density mesh: 0.05–0.10 mm; Machine room air conditioner filter mesh II: 0.15–0.20 mm;
Physical Properties Testing
Physical property testing of PP filter media primarily focuses on mechanical strength and durability, specifically including the following items:
First, tensile property testing (including tensile strength and elongation at break) aims to verify the material's resistance to damage during installation and use (such as cutting and exposure to air pressure). Testing methods follow GB/T 1040.3-2006 "Plastics—Determination of Tensile Properties—Part 3: Test Conditions for Films and Sheets." Tensile strength testing must be conducted according to application-specific requirements: — For standard PP filter materials: longitudinal tensile strength ≥1.5MPa, transverse ≥1.0MPa. Materials used in high-wind-pressure applications (e.g., industrial fan filters) require longitudinal tensile strength ≥2.0MPa to prevent tearing under wind pressure. Testing may involve either cutting a 150mm×25mm standard specimen and stretching it at 50mm/min using a universal tensile testing machine, or cutting a 30mm-wide specimen along the longitudinal direction and stretching it at the same speed while recording the maximum tensile force;
Second, burst strength testing: Place the filter mesh horizontally. Apply vertical downward pressure to the center of the mesh using a push-pull gauge with a disc-shaped thrust terminal until rupture occurs. Record the pressure value at rupture, which must be ≥70N. Third, bending performance testing: Simulate the installation scenario by assembling and disassembling the sample 20 times. The sample must show no signs of delamination, cracking, or fracture.
Filter Efficiency and Resistance Characteristics Testing
Core Performance Metrics for Validating Particle Capture Capacity and Airflow Resistance of Filter Materials:
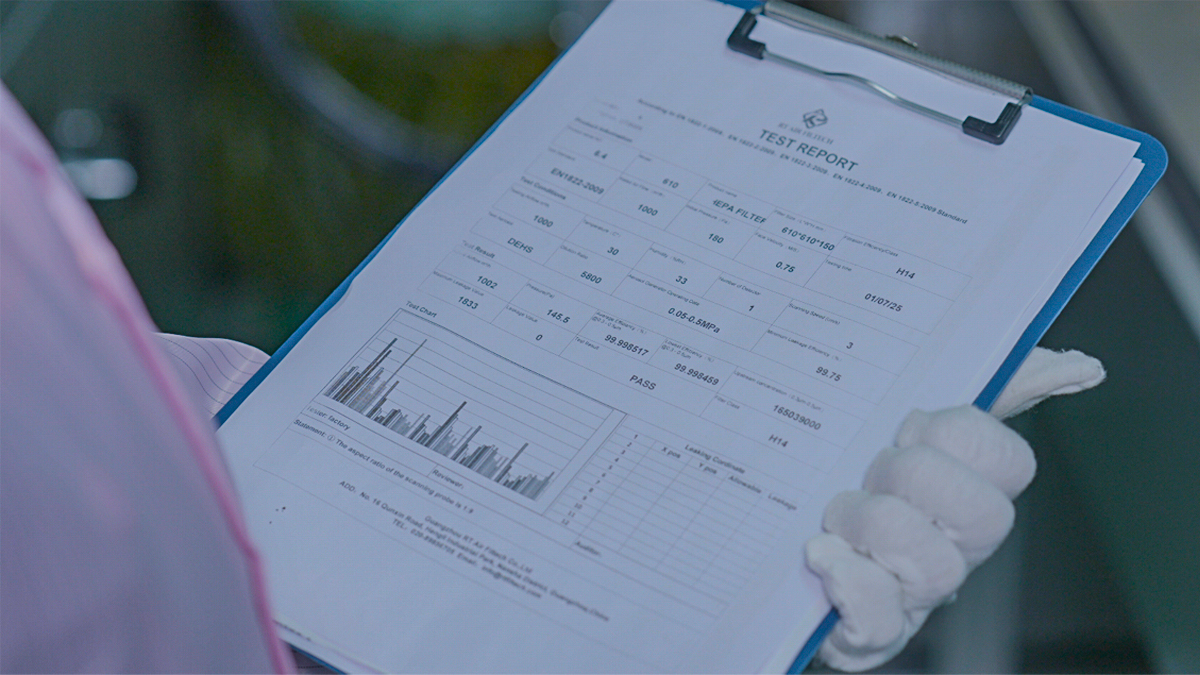
Filter Efficiency: Employing the laser particle counter method, aerosols with multi- or mono-dispersed particle sizes (e.g., 0.3μm, 0.5μm particles) are generated using a Laskin nozzle atomization system. Simultaneous detection of particle concentrations upstream and downstream of the sample calculates the filtration efficiency (e.g., ≥99.95% indicates high-efficiency filter material). Compliant standards include GB 2626-2019, EN1822-3:2009, ISO 29463-3:2011, etc.;
Resistance Characteristics: Measures the pressure differential (ΔP) across the sample using a differential pressure sensor, calculating the resistance per unit area (ΔP/S, unit: Pa/m²). Resistance values must meet application requirements; low-resistance, high-efficiency filtration materials typically exhibit resistance ≤100 Pa.
Flame Retardant Performance Testing
PP (polypropylene), being a flammable material, requires the addition of flame retardants (such as bromine-antimony systems, nitrogen-phosphorus systems, intumescent flame retardants, etc.) to enhance its flame-retardant properties. The UL94 vertical burning test is the most commonly used method for evaluating flame retardancy. It simulates the combustion behavior of materials under flame exposure to assess their self-extinguishing capability, burning rate, and dripping risk.
The most widely applied plastic flame retardant rating standards are categorized as HB (horizontal burning), V-0/V-1/V-2 (vertical burning), and 5VA/5VB (enhanced requirements). During testing, the specimen (with specified thickness, e.g., 3–13 mm) is vertically secured and ignited with a defined flame (e.g., V-0 grade flame height 8.5 mm) for 10 seconds. After removal, the burning time with flame (not exceeding 60 seconds per ignition) is recorded. This ignition is repeated five times while observing whether molten droplets ignite the underlying cotton wool. For example: - V-0 requires flame extinction within 30 seconds after two ignitions with no molten droplets - V-2 permits molten droplets but prohibits ignition of the cotton wool
In PP air filter material testing, which items are most likely to fail inspection?
|
Test Items |
Reason for non-compliance |
Improvements |
|---|---|---|
|
Filtration Efficiency |
|
|
|
Leak |
|
Enhance visual inspections of raw materials and finished products, and conduct leak detection tests on each unit (smoke tests). |
|
Initial resistance |
|
|
|
Dimensions and Appearance |
Production process control is not stringent, resulting in dimensional deviations or cosmetic defects. |
Strictly enforce production standards and strengthen pre-shipment inspections. |
How to Reduce the Defect Rate?
To improve the pass rate of PP air filter materials, efforts must be made at both the source and process stages:
Strictly control raw material quality: The quality of filter media is fundamental to determining the performance of the finished product. Some companies use low-cost filter paper to reduce costs, which directly leads to difficulties in meeting standards for filtration efficiency and resistance. Therefore, establishing standardized raw material inspection procedures is crucial.
Refine production and quality inspection systems: Many manufacturers lack essential testing equipment and quality control frameworks. It is recommended to invest in basic testing equipment like smoke test benches, conduct random sampling or even unit-by-unit inspection for each batch of incoming materials and finished products, and meticulously record data such as air velocity and particle counts. Simultaneously, develop standard operating procedures, particularly for critical workstations like filter material cutting, pleating, and bonding/sealing to frames, ensuring consistent and standardized operations.
RT Air Filtech consistently treats quality as our lifeline, committed to becoming the most trusted one-stop air filter manufacturer for global customers. From core filter media R&D to intelligent filter manufacturing, we rigorously implement quality control at every stage to ensure every delivered product delivers outstanding performance and reliable safety.
We understand that quality is not merely a standard—it is a commitment. Moving forward, RT Air Filtech will continue to be driven by innovation and customer-centricity, delivering more efficient and stable air filtration solutions to safeguard clean air in every corner of the world.
Your Air, RT Cares.
Let's breathe together toward a cleaner future.
To learn more about our quality control system or customized solutions, feel free to contact our professional team anytime.